
Tube Laser Cutting
Our laser tube cutting service cuts tube and pipe profiles for frames, brackets, fixtures, and weldments. Have questions about your design? Reach out anytime at
At a glance
- +/- 0.005" tolerance on overall dimensions
- Precision laser tolerance for repeatable tube features
- End-cut planes must be at least 45 degrees from the tube centerline
- Straight tube members only; pre-bent or curved tube is not supported
- Holes on square and rectangular tube keep at least half the wall thickness from the side walls (details)
- Holes and cutouts should be at least half as wide as the tube wall is thick (details)
- Steel, stainless steel, and aluminum public tube profiles
- Holes, slots, miters, coping, and tube end profiles
Tube materials
Available public tube profiles for laser tube cutting in steel, stainless steel, and aluminum. Download nominal STEP/DXF reference geometry; confirm unspecified corner radii before designing mating fits.
Loading tube profiles…
Outer size is OD for round tube or width × height for rectangular tube. Wall = nominal wall thickness. Corner R = outside corner radius. “Not specified” means the stock radius is unconfirmed; sharp corners in reference CAD do not specify the supplied stock. Confirm corner dimensions with us if they affect fit. Contact support for other sizes, materials, or wall thicknesses.
Design Guidelines
Tolerances
Laser cut tube parts use a precision laser tolerance of +/- 0.005" on overall dimensions. Tolerance stack-up can vary with long tube lengths and weldment fit-up.
End Cuts and Miters
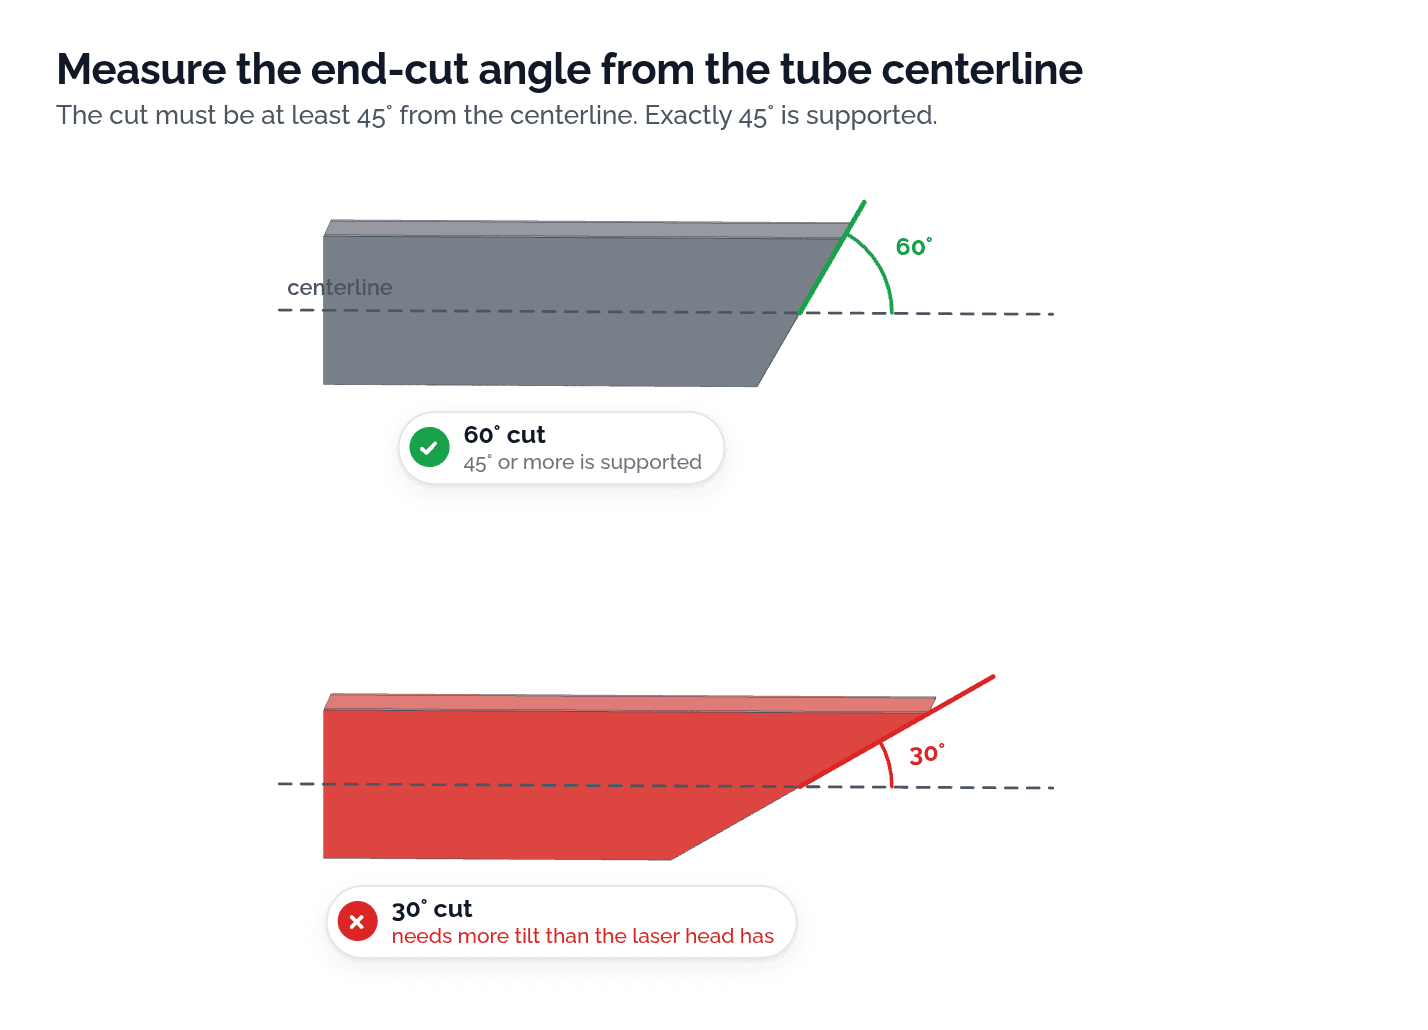
Measure the end-cut plane from the local tube centerline. The angle must be at least 45 degrees; only cuts below 45 degrees are unsupported. Bevel direction and fit-up should be clear in the uploaded STEP model.
Holes and Slots
Make holes and slots at least half as wide as the tube wall is thick, and keep them clear of the corners: at least half the wall thickness of flat tube between the hole edge and the inside of the side wall. Larger holes generally produce cleaner, more repeatable tube parts.
Tube Profiles
Quote against the active public tube profiles shown above. If you need a different tube size, material, or wall thickness, contact support before quoting.
End-cut angle limit
A square end cut is 90 degrees from the tube centerline. As the cut becomes more acute, the laser head must tilt farther. Designs with an end-cut plane below 45 degrees are blocked during quoting.
Straight tube only
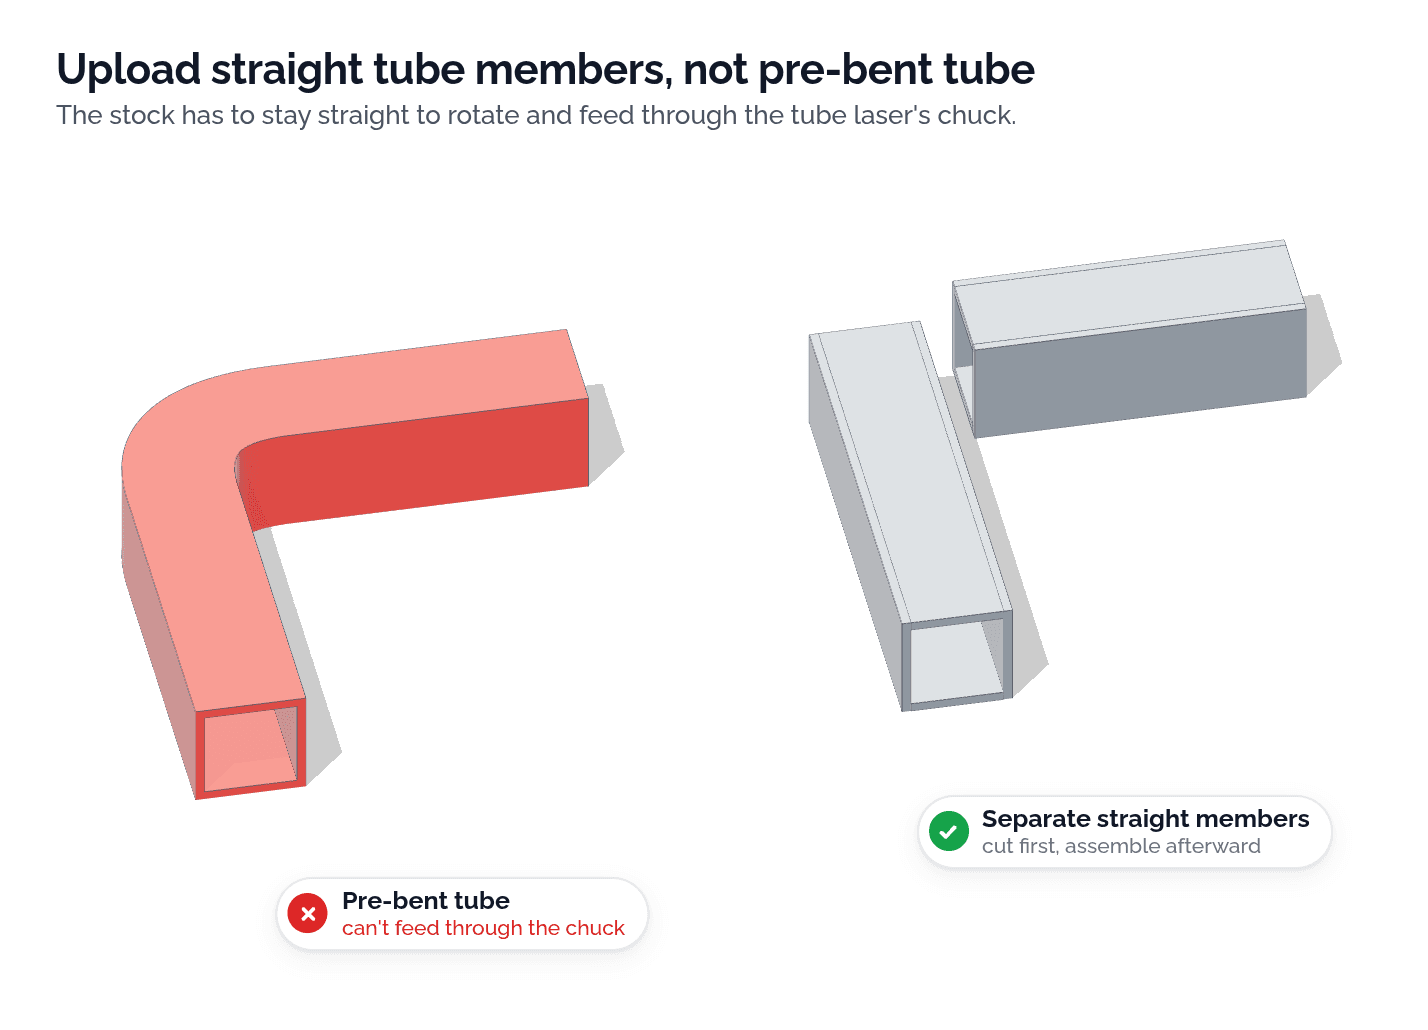
Pre-bent and curved tube cannot rotate or feed through the tube-laser chuck. Upload the straight members as separate parts, then join or bend them in a later manufacturing step.
Hole clearance from side walls
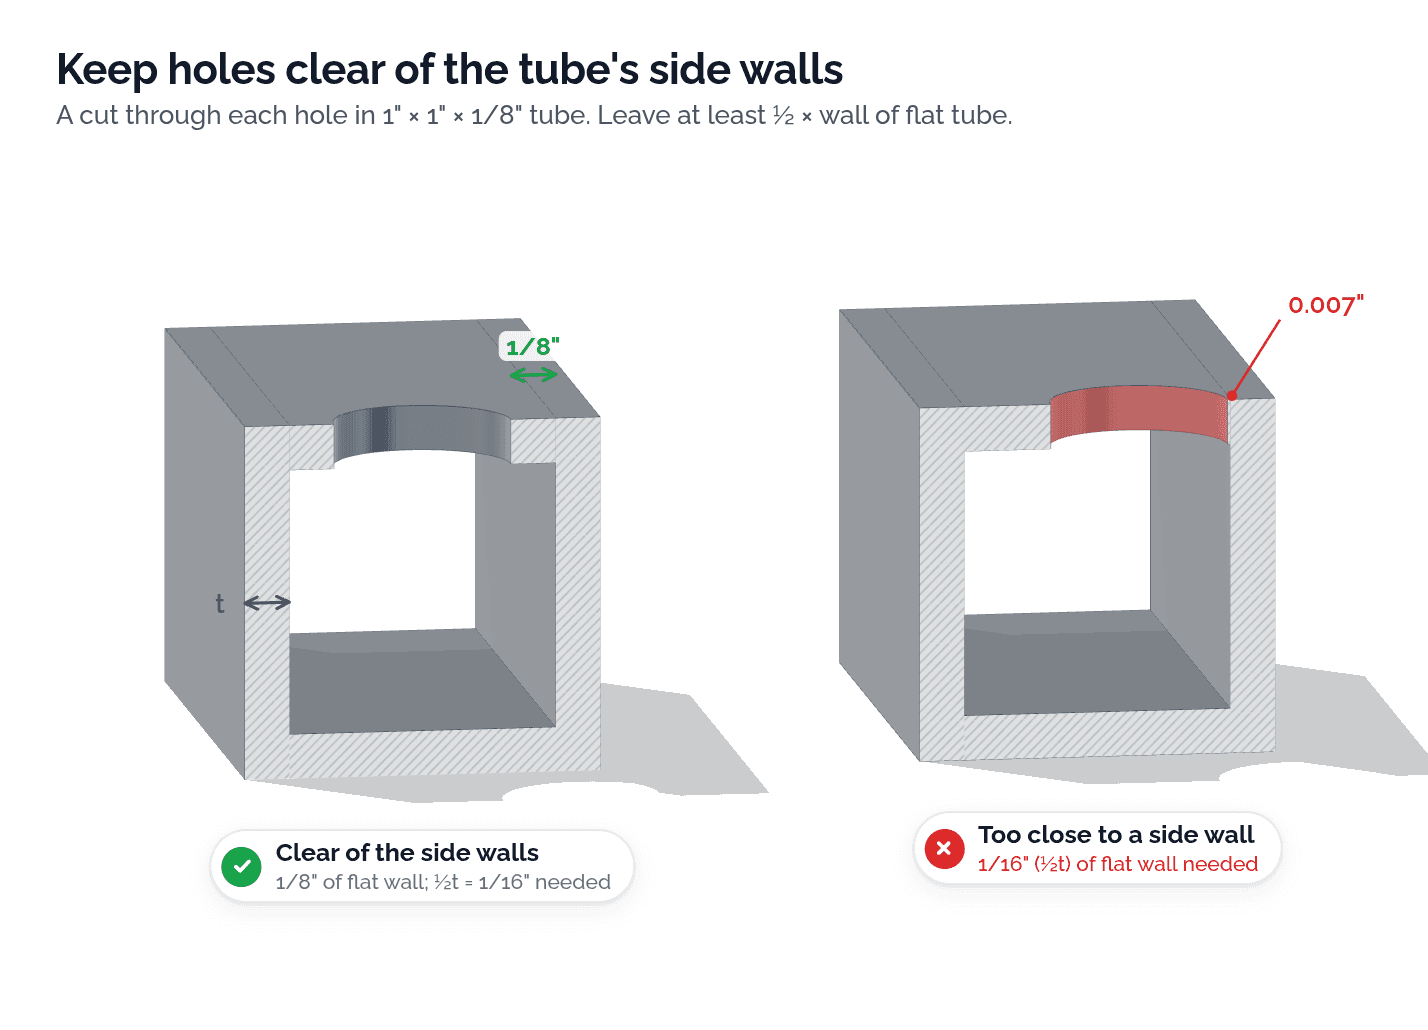
On square and rectangular tube, the laser cuts a through hole straight through one wall. If the hole reaches into the corner, the beam also cuts the perpendicular wall, notching the corner and distorting the hole. Keep at least half the wall thickness of flat tube between the edge of the hole and the inside face of the side wall. On 1" x 1" tube with a 1/8" wall, that leaves a 0.625" wide band down the middle of each face for holes.
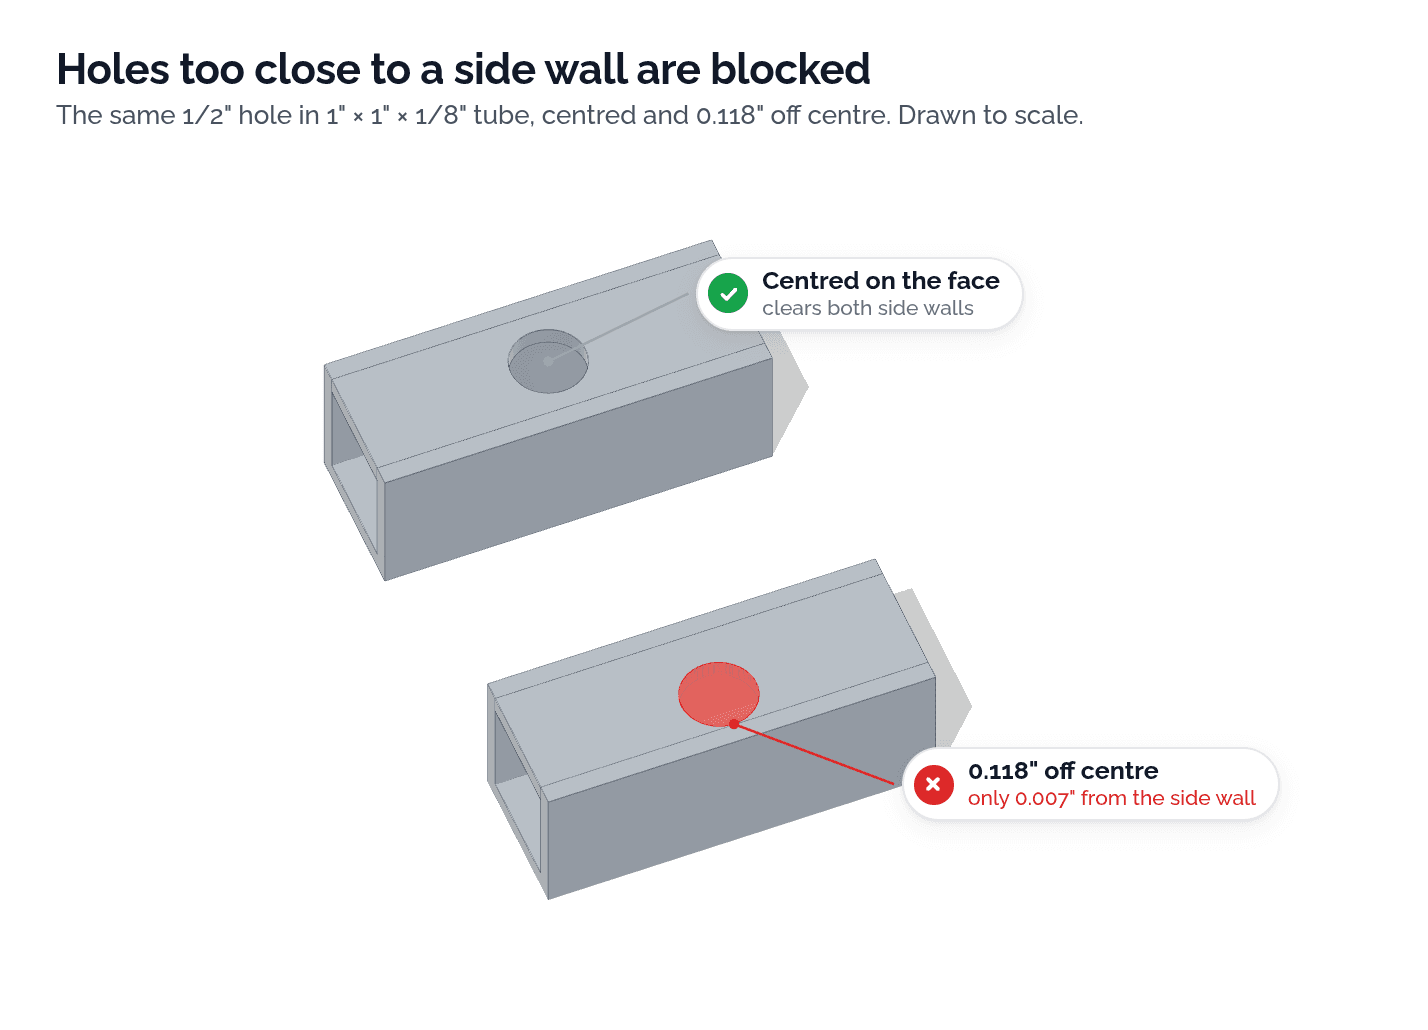
Quotes with a hole closer than this are blocked. Move the hole toward the middle of its face, make it smaller, or choose a larger tube. Rectangular cutouts are checked by their shorter side; contact support about irregular cutouts near a corner.
Features smaller than half the wall thickness
As on sheet parts, a hole or cutout should be at least half as wide as the thickness of the wall it is cut through. Narrower features can taper, carry slag, or come out undersized. You can still order them by accepting the risk when you quote. For channel, angle, and wide-flange shapes, the thinner of the web and flange is used.
Supported Materials
Laser tube cutting is available for steel, stainless steel, and aluminum tube profiles. Material availability depends on active public tube inventory and may change as new profiles are added.
Files and Review
Upload a STEP file with the tube profile, length, holes, slots, end cuts, and bevels modeled as you want them manufactured. We review submitted parts for manufacturability and will contact you if we spot an issue.
Can't find the tube profile you need, or unsure whether a bevel or feature is manufacturable? Reach out anytime at